2026 Top Lyophilization Equipment Manufacturers?
Choosing among the 2026 Top Lyophilization Equipment Manufacturers requires more than comparing catalog prices or chamber sizes. Freeze-drying performance depends on vacuum stability, condenser capacity, shelf uniformity, control software, and service response. A reliable system should maintain consistent temperatures across loaded shelves, even during demanding cycles. Small details matter. Door seals, sensor calibration, and cleaning access can affect production results.
This guide examines Lyophilization Equipment Manufacturers through a practical and evidence-based lens. It considers equipment design, validation support, operator experience, documentation quality, and long-term maintenance. Manufacturers serving pharmaceutical, biotechnology, food, and research applications may offer very different strengths. One company may excel in aseptic production, while another provides flexible laboratory systems or stronger regional support. Published specifications help, but they do not tell the whole story. Site references, factory testing, installation records, and customer feedback deserve equal attention.
There is no universal winner. That is worth remembering. A high-capacity unit may be unsuitable for a small development laboratory. Likewise, a lower purchase price can hide costly upgrades, training gaps, or delayed spare parts. Some comparisons also rely too heavily on marketing language. This guide attempts to avoid that weakness by focusing on measurable capabilities and realistic operating conditions. Readers should still verify current certifications, local service coverage, compliance requirements, and total ownership costs before making a final decision. Good equipment protects product quality. Good judgment protects the investment.
What Is Lyophilization Equipment and Why Does It Matter in 2026?
What Is Lyophilization Equipment and Why Does It Matter in 2026?
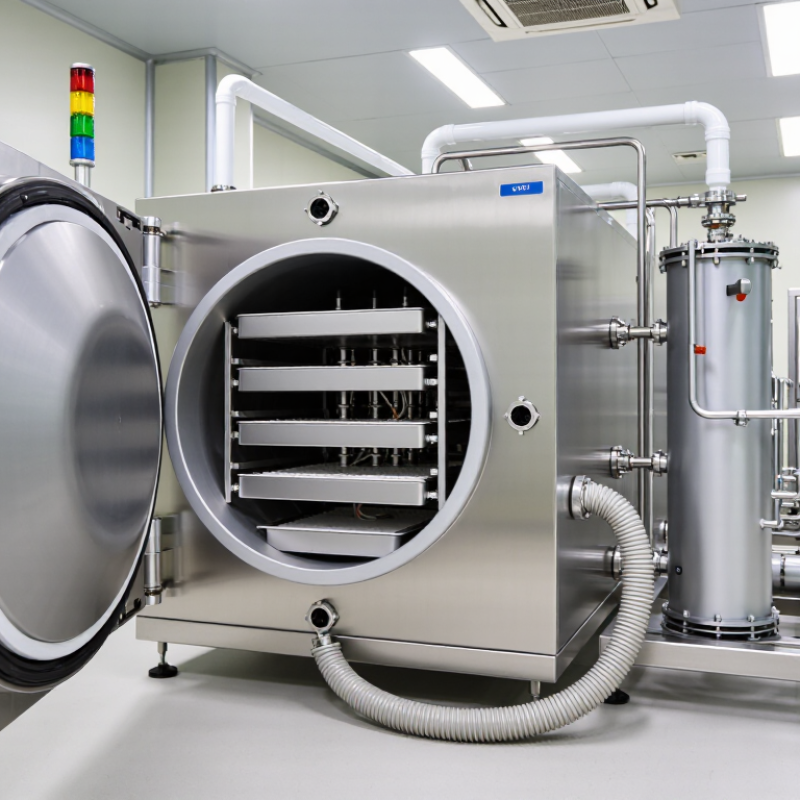
Lyophilization equipment removes water from sensitive products through freezing, vacuum, and controlled heating. The process protects structure, stability, and shelf life without relying on harsh temperatures. In 2026, manufacturers need equipment that supports consistent cycles, energy awareness, and stronger data control. A modern system may include cleanable chambers, shelf temperature sensors, condenser protection, and automated recipe management. Small temperature changes can affect the final cake appearance and reconstitution time. That detail matters.
Choosing among top lyophilization equipment manufacturers requires more than comparing chamber size or purchase price. Experienced teams should review validation support, calibration practices, operator training, and maintenance response. Equipment must also fit the facility’s utilities, containment needs, batch volume, and quality procedures. Reliable suppliers provide clear performance data and documented testing methods. However, no system is perfect. Unexpected heat transfer differences can still appear during scale-up, so pilot trials and continued monitoring remain necessary.
Tips: Ask for cycle-development evidence, not only attractive specifications. Inspect product-contact materials and cleaning access. Check how alarms are recorded and reviewed. Test data integrity before routine production. Leave room for human judgment; automation helps, but it does not replace trained operators. A practical factory visit can reveal awkward valves, poor visibility, or difficult maintenance points that brochures rarely show.
2026 Top Lyophilization Equipment Manufacturers? - What Is Lyophilization Equipment and Why Does It Matter in 2026?
Company-neutral comparison of major lyophilization equipment categories and practical selection criteria
| Equipment Category | Typical Production Scale | Typical Shelf-Temperature Range | Typical Condenser Temperature | Typical Chamber Pressure | Common Applications | Key 2026 Evaluation Criteria |
|---|---|---|---|---|---|---|
| Laboratory Benchtop Freeze Dryer | Approximately 1–10 L of ice capacity | About −40°C to +60°C, depending on product and cycle stage | Typically −50°C to −85°C | Commonly below 0.5 mbar during primary drying | Research, formulation screening, analytical development, and small clinical batches | Compact footprint, recipe development, data logging, easy cleaning, and low operating cost |
| Pilot-Scale Shelf Freeze Dryer | Approximately 10–100 L of ice capacity | About −40°C to +60°C | Typically −60°C to −85°C | Commonly 0.05–0.5 mbar during primary drying | Scale-up studies, process characterization, clinical manufacturing, and engineering batches | Scale-up similarity, shelf uniformity, automated control, product-temperature monitoring, and recipe transfer |
| Production Pharmaceutical Freeze Dryer | Approximately 100–2,000+ L of ice capacity | About −50°C to +70°C, based on formulation requirements | Typically −70°C to −85°C | Often approximately 0.01–0.2 mbar during primary drying | Commercial vaccines, biologics, injectable drugs, and high-value sterile products | GMP compliance, aseptic integration, validated control systems, containment, throughput, and energy efficiency |
| Manifold Freeze Dryer | Small-volume vials or flasks; generally non-production scale | Usually controlled through external freezing and ambient laboratory conditions | Typically −50°C to −85°C | Commonly below 0.1 mbar | Microbiology, laboratory samples, diagnostic materials, and non-sterile research work | Low initial cost, simple operation, sample flexibility, and rapid access to vacuum drying |
| Stoppering Freeze Dryer | Small laboratory units through large commercial systems | Approximately −50°C to +70°C | Typically −60°C to −85°C | Commonly 0.01–0.2 mbar during primary drying | Sterile injectable products requiring vial stoppering under controlled conditions | Aseptic chamber design, automatic stoppering, sterile transfer, leak integrity, and contamination control |
| Bulk Freeze Dryer | From several kilograms to industrial-scale batches | Typically about −40°C to +60°C | Usually −50°C to −80°C | Often 0.05–0.5 mbar | Food ingredients, diagnostics, biotechnology intermediates, and bulk pharmaceutical materials | Loading and unloading efficiency, material handling, uniform drying, cleaning strategy, and batch traceability |
| Continuous or Semi-Continuous Lyophilization System | Application-dependent; designed for repeated or near-continuous product flow | Controlled across freezing, primary drying, and secondary drying zones | Typically below −50°C, depending on condenser and product design | Usually maintained below atmospheric pressure throughout drying | High-throughput products, advanced manufacturing research, and reduced hold-time processes | Process intensification, automated material flow, residence-time control, digital monitoring, and reduced footprint |
| Aseptic Integrated Lyophilization Line | Commercial vial, syringe, or cartridge production lines | Commonly about −50°C to +70°C, validated for the specific formulation | Typically −70°C to −85°C | Commonly 0.01–0.2 mbar during primary drying | Sterile biologics, vaccines, complex injectables, and temperature-sensitive medicines | Isolator or restricted-access integration, electronic batch records, serialization readiness, robotic handling, and regulatory data integrity |
Related Posts
-
How to Choose a Pharmaceutical Lyophilizer in 2026?
-
Why Choose a Pharmaceutical Lyophilizer for Your Facility?
-
Top 10 Lyophilization Machines You Should Know About?
-
Top Uses and Benefits of High Performance Liquid Chromatography in Research?
-
2026 How to Choose the Best Peptide Synthesizer Machine?
-
Why Choosing the Right Lyophilization Equipment Manufacturers Matters?