skip to content

How to Choose the Best Pharmaceutical Lyophilizer?

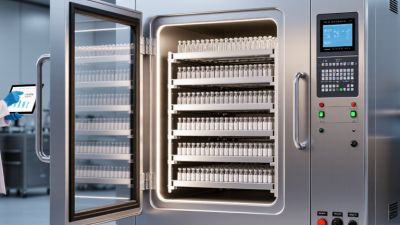
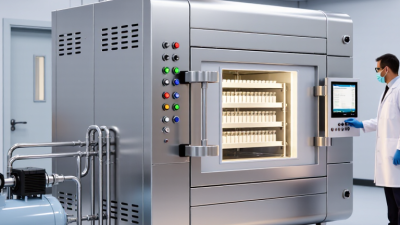
Choosing a Pharmaceutical Lyophilizer requires more than comparing chamber size and purchase price. It affects product stability, sterility assurance, cycle time, and long-term operating costs. In practice, the right machine rarely looks perfect on paper.

Industry demand is expanding. Grand View Research’s 2024 lyophilization equipment analysis identifies biologics, vaccines, and injectable medicines as major growth drivers. MarketsandMarkets also reports increasing demand for advanced freeze-drying systems, supported by rising biopharmaceutical production and stricter quality expectations. These trends matter, but market growth alone should not determine your specification.

A reliable evaluation starts with the product. Consider vial configuration, fill volume, formulation sensitivity, target residual moisture, and required shelf life. The FDA’s Process Validation guidance emphasizes scientific understanding, measurable controls, and continued process verification. PDA Technical Report No. 60 similarly highlights the importance of cycle development, equipment qualification, and contamination control. A glossy brochure cannot replace those controls.

Look closely at condenser capacity, shelf uniformity, vacuum performance, cleanability, automated loading, and data integrity. Ask for documented heat-transfer results, not general promises. Review factory acceptance testing and service response times. Small details matter, such as how quickly shelves recover after loading or how easily operators inspect door seals.

There is no universal best model. A compact laboratory unit may suit development work but fail during commercial expansion. An oversized system may create unnecessary energy and maintenance costs. That mistake happens.

The strongest choice connects formulation science, regulatory expectations, operator experience, and total lifecycle cost. Independent qualification support is valuable. So is admitting what remains uncertain before signing the purchase order.
How to Choose the Best Pharmaceutical Lyophilizer?

Define the Product and Process Requirements

How to Choose the Best Pharmaceutical Lyophilizer?

Define the Product and Process Requirements

Choosing a pharmaceutical lyophilizer starts with the product, not the equipment brochure. Define the formulation’s concentration, fill volume, vial size, and active ingredient sensitivity. Record the glass transition temperature and collapse temperature when available. These values guide shelf temperature and chamber pressure decisions.

Product behavior can change during freezing. Ice crystal structure affects drying time and cake appearance. A protein solution may need controlled nucleation and gentle temperature ramps. A small-volume injectable may require different loading patterns than a larger batch. Test representative samples, not only ideal laboratory batches. Reality is less tidy.

The process requirements should include batch size, target cycle time, loading configuration, and acceptable residual moisture. Specify whether the system needs automatic loading, recipe control, clean-in-place functions, or sterilization support. Reliable temperature and pressure sensors are essential for tracking critical process parameters. Data should be traceable, reviewable, and protected from accidental changes.

Scale-up deserves careful attention. Shelf spacing, condenser capacity, and heat transfer may behave differently in a larger chamber. A cycle that works in a development unit can fail during production. Build margins into the design, but avoid excessive capacity that increases cost and energy use. Review validation needs early, including alarms, calibration, leak testing, and documentation. One overlooked detail can delay an otherwise sound project.

Compare Lyophilizer Types and Key Operating Features

Choosing the Best Pharmaceutical Lyophilizer

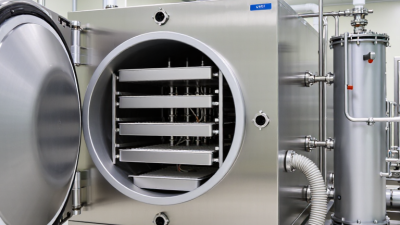
Choosing the best pharmaceutical lyophilizer starts with product behavior, not chamber size. Tray or shelf lyophilizers suit controlled batch processing of vials. They provide precise shelf temperature and chamber pressure control. Manifold units support small development runs, but they expose containers directly to the vacuum path. That can complicate scale-up. Rotary systems may suit specialized liquid handling applications, although vial production requires different loading and stoppering arrangements. Compare fill volume, freezing sensitivity, cake structure, and target batch size.

Review shelf temperature uniformity across the chamber. A few degrees can change ice sublimation and residual moisture. Check condenser temperature, ice capacity, and pull-down speed under realistic loads. Vacuum control should remain stable during primary drying, not only during empty-chamber testing. Automatic stoppering, clean-in-place support, sterilize-in-place capability, and secure recipe control matter in routine production. Reliable data logging should capture pressure, shelf temperature, product temperature, alarms, and cycle changes.

For development, prioritize flexible shelves, accurate probes, and recipes transferable to larger equipment. For commercial use, assess loading ergonomics, maintenance access, utility demand, and validated control functions. Do not judge performance from brochure specifications alone. Performance varies. Request mapping data and a representative cycle trial. A machine may reach very low pressure yet dry unevenly. I have seen teams overvalue condenser capacity and undervalue heat transfer. That mistake is easy to repeat.

How to Choose the Best Pharmaceutical Lyophilizer? - Compare Lyophilizer Types and Key Operating Features

Lyophilizer Type Typical Shelf Area Typical Batch Scale Primary Application Condenser Temperature Typical Chamber Pressure Range Key Operating Features Main Selection Consideration
Laboratory Benchtop Approximately 0.1–1.0 m² Milligrams to several liters of solution Formulation development, cycle development, and small-scale research About −50°C to −85°C Typically 5–200 mTorr Compact footprint, basic shelf temperature control, optional stoppering, and limited automation Choose when flexibility, low product consumption, and fast experimentation are more important than throughput
Pilot-Scale Approximately 1–10 m² Several liters to hundreds of liters of solution Scale-up studies, process characterization, and clinical or engineering batches About −60°C to −85°C Typically 20–200 mTorr Improved shelf uniformity, controlled ramping, recipe storage, data logging, and optional automated stoppering Choose when the equipment must support reliable scale-up and generate process data comparable with production units
Production-Scale Batch Approximately 10–100+ m² Hundreds to thousands of liters of solution Commercial manufacturing of sterile injectable and other temperature-sensitive products About −70°C to −85°C Typically 50–250 mTorr Automated recipes, validated data acquisition, controlled nucleation options, automatic stoppering, and cleanable product-contact surfaces Choose based on required annual capacity, loading configuration, cycle time, validation strategy, and facility utilities
Manifold Freeze Dryer No internal shelf area; external flask or vial connections Small laboratory quantities Research samples, bulk materials, and non-sterile development work About −50°C to −85°C Typically below 200 mTorr Simple operation, external containers, low capital cost, and limited control of heat transfer Choose only when aseptic vial processing, precise shelf control, and commercial process similarity are not essential
Aseptic Shelf Lyophilizer Laboratory to production scale Sterile vial batches from development to commercial scale Sterile injectable pharmaceuticals and biologics Usually −60°C to −85°C Typically 50–200 mTorr Sterile chamber design, validated sterilization, automatic stoppering, filtered gas admission, and controlled loading/unloading Choose when sterility assurance, contamination control, and regulatory compliance are critical requirements
Bulk Lyophilizer Varies by chamber and tray configuration Bulk solids or concentrated product in trays Bulk active ingredients, excipients, diagnostics, and materials not filled directly into final containers About −50°C to −85°C Typically 50–300 mTorr Large tray capacity, product containment, controlled discharge, and options for inert-gas backfill Choose when high bulk capacity and material recovery are more important than direct vial stoppering
Important: The values shown are typical engineering ranges rather than universal specifications. Actual performance depends on formulation, fill volume, container geometry, shelf loading, heat-transfer characteristics, condenser capacity, vacuum-system design, and the validated process cycle.

Evaluate Capacity, Shelf Design, and Freeze-Drying Performance

How to Choose the Best Pharmaceutical Lyophilizer?
Evaluate Capacity, Shelf Design, and Freeze-Drying Performance

Capacity should match your actual batch size, not an optimistic production forecast. A chamber packed too tightly can restrict vapor movement and create uneven drying. Check usable shelf area, not only the advertised chamber volume. Leave room for trays, sensors, and safe loading access. A small pilot load may look efficient, yet it can hide scale-up problems.

Shelf design directly affects heat transfer. Shelves should maintain consistent temperature across their surfaces. Ask for temperature uniformity data under loaded conditions. Empty-chamber results are useful, but they do not represent real production. I have seen edge vials dry differently from center vials. That detail can become costly. Flexible shelf spacing also supports different container heights and filling volumes. Fixed spacing may limit future products.

Freeze-drying performance depends on condenser capacity, vacuum control, and precise cycle management. Compare sublimation rates, condenser temperature, and pressure stability during representative tests. Review how the system records product temperature and endpoint data. Reliable sensors matter more than impressive specifications. A cycle that finishes quickly is not automatically better. Product appearance, residual moisture, reconstitution time, and activity must remain acceptable. Some evaluations still rely on one successful run. That is not enough. Repeat testing with varied loads can reveal weaknesses before routine manufacturing begins.

Assess Containment, Cleaning, Automation, and Validation Needs

Choosing the Best Pharmaceutical Lyophilizer

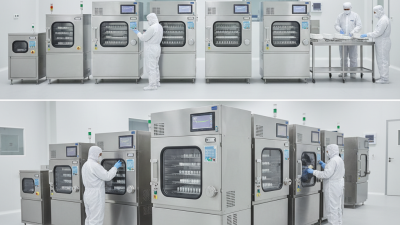
Choosing a pharmaceutical lyophilizer starts with the product, not the machine. Containment requirements should reflect potency, exposure risk, and operator movement. Ask where particles could escape: during loading, unloading, or filter replacement. A sealed transfer path, pressure monitoring, and accessible glove ports can reduce risk. Small gaps matter. Walk through the room with operators before approving the layout. Their practical observations often reveal issues missed in drawings.

Cleaning capability deserves equal attention. Review chamber geometry, drain points, spray coverage, and residue sampling locations. A narrow valve or shadowed shelf can retain material after a seemingly successful cycle. Request evidence from representative soils, not only clean water tests. Manual cleaning may look flexible, but it can vary between shifts. I have seen strong procedures fail when access was uncomfortable. That weakness belongs in the design review.

Automation should make critical steps visible. Trend shelf temperature, chamber pressure, condenser performance, and alarms with secure records. Avoid adding software features without a clear process purpose. More screens do not guarantee better control. Validation must connect user requirements to risks, tests, and acceptance criteria. Challenge hold times, sensor calibration, recipe permissions, and recovery after power interruption. Some assumptions will be wrong. Document them, test them, and revise the plan before routine production begins.

Review Compliance, Lifecycle Costs, Service, and Supplier Support

Choosing a pharmaceutical lyophilizer requires more than comparing chamber volume or condenser capacity. Compliance must be visible in daily operation. Review electronic records, audit trails, recipe controls, and data-integrity safeguards against 21 CFR Part 11 and EU GMP expectations.

The FDA Drug Shortages Task Force reported in 2019 that manufacturing and product-quality problems contributed to 62% of shortages studied. That figure deserves attention. Ask whether the supplier provides documented IQ, OQ, and performance qualification support. Review chamber mapping, leak testing, sterilization evidence, and contamination-control procedures. A polished factory acceptance test is useful, but site acceptance often reveals the real weaknesses.

Purchase price can mislead. Build a ten-year lifecycle model covering utilities, validation, preventive maintenance, calibration, spare parts, software upgrades, operator training, and production downtime. ISPE’s Pharma 4.0 guidance highlights data connectivity and scalable automation as important maturity factors. Still, advanced software is not automatically better. It may create more validation work. Service quality matters just as much. Request guaranteed response times, local technical coverage, critical-part availability, and documented escalation routes. Speak with current users, not only reference contacts selected by the supplier. My checklist remains imperfect; unexpected downtime and difficult recipe transfers are hard to price. That uncertainty should be recorded, challenged, and periodically reviewed.